Issue Summary: When the surface lies, how do you know what's inside?
In most manufacturing environments, "good enough" data is the enemy of true quality. We rely on sensors to tell us if a part is within tolerance, and we trust those numbers because they are easy to read on a dashboard. But there is a massive gap between a signal that looks correct and a physical state that is actually stable.
Currently, many of our inspection methods are blind to what happens at the material level. We measure intensity—how much light hits a sensor or how much pressure is registered—but we ignore the underlying coherence and phase data. This means we might be passing parts that look perfect on the line but contain internal structural flaws that will cause them to fail six months into their service life.
The solution isn't just "better" sensors; it’s a shift in how we capture information. By moving toward photonic-based sensing, we can separate overlapping signal modes. This allows us to see through the surface noise and identify the internal physical states that actually dictate long-term reliability. We need to stop looking at what the part looks like and start seeing what it is.
The Hidden Flaw: Why 'Intensity' Isn't Enough Data
I’ve spent enough time on production floors to know that most people trust a green light because they have no reason not to. If the sensor says the intensity is within spec, the part moves forward. We call this "passing," but in many cases, it is actually The Intensity Illusion.
Quality is not just about hitting a target number; it is about understanding the physics of why that number was hit. When we rely solely on basic intensity measurements, we are essentially looking at a shadow and trying to guess the shape of the object casting it. You can have two different physical states—one stable and one drifting toward failure—that produce the exact same intensity reading.
The industry has settled for this because intensity is easy to quantify and even easier to automate. It fits neatly into a spreadsheet. But when you ignore phase data and signal coherence, you are ignoring the "why" behind the measurement. You are missing the subtle shifts in material behavior that precede a catastrophic failure. A plan on paper that only monitors surface-level metrics is not a quality plan; it is a gamble on whether the hidden variables will behave themselves today.
Why We Accept Less Than Perfect Information (And How That Habit Costs Money)
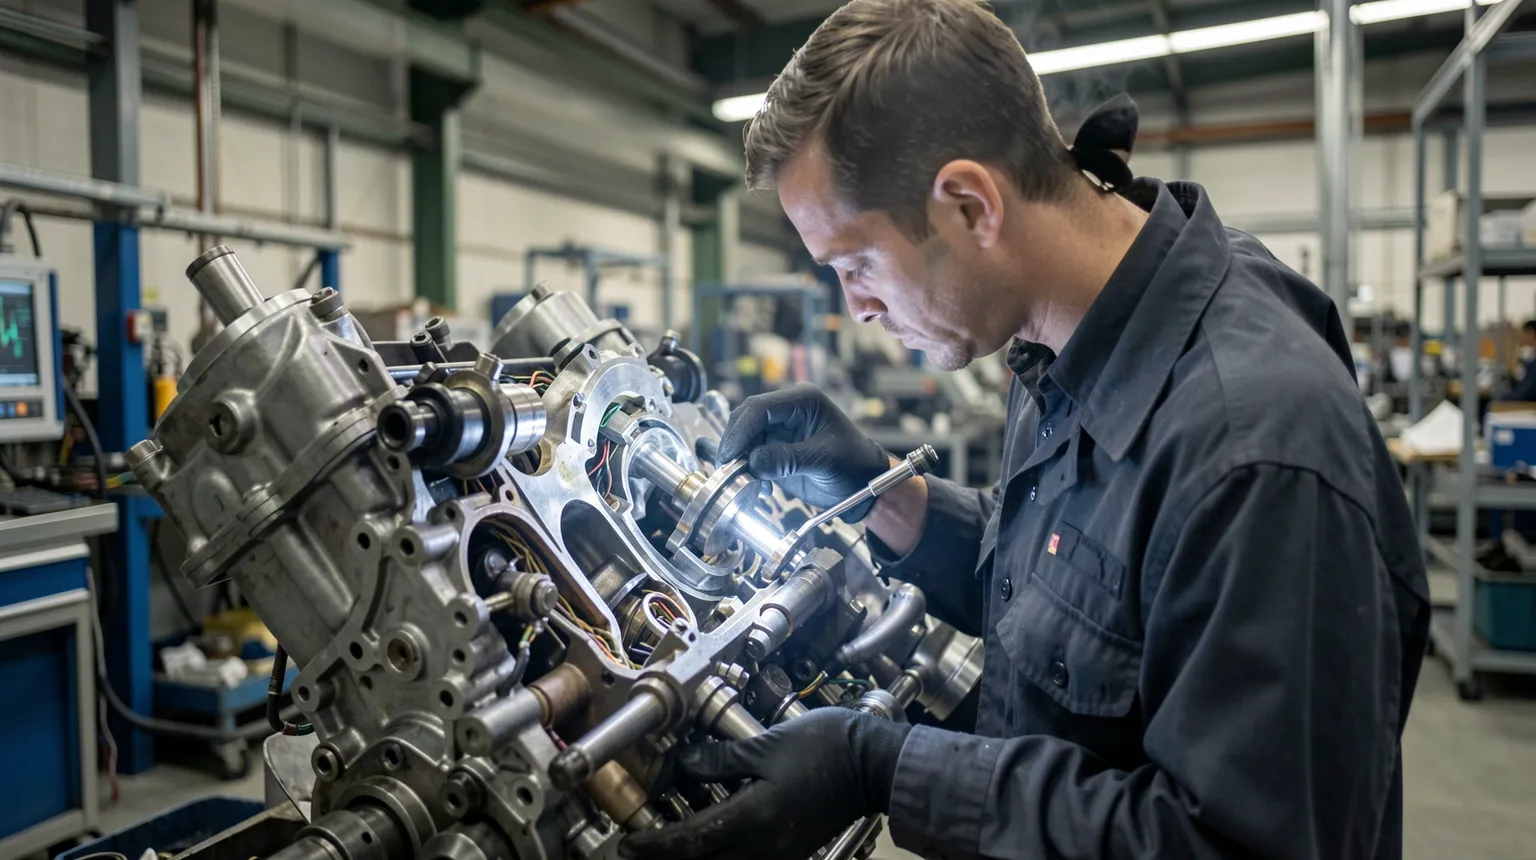
We settle for "good enough" data because of a fundamental human bias toward the path of least resistance. It takes effort to interpret complex signal modes, but it takes almost no effort to watch an intensity gauge. We choose the comfort of known limitations over the complexity of true visibility.
This habit is not just an engineering oversight; it's a cultural choice to prioritize "motion mistaken for progress." If we can see enough data to make the line keep moving today, we assume that is sufficient. But this creates a dangerous gap between our perceived reality and the actual state of the product.
| The Comfortable Rationalization | The Underlying Reality |
|---|---|
| "The sensor says it's in spec; the part is good." | The internal material structure is drifting toward fatigue despite stable surface readings. |
| "We don't need more complex data; it complicates the process." | We are intentionally ignoring the variables that cause 90% of our field failures. |
| "The current sampling rate is sufficient for our needs." | We are capturing a snapshot of intensity while missing the high-frequency phase shifts that signal instability. |
| "It's too expensive to upgrade the sensing suite now." | The cost of an invisible defect appearing in the field will be ten times higher than the cost of better data today. |
The Real Cost: The Price of Invisible Variation
When we ignore what happens at the material level, we aren't just risking a minor defect—we are inviting catastrophic failure. There is a massive difference between an "obvious" defect that can be caught by a human eye and "invisible variation" caused by internal shifts in signal coherence.
The cost of this ignorance manifests in three specific ways:
- Delayed Detection: We find out the part failed when it's already in the customer’s hands, not on our line.
- Unpredictable Recalls: Because we didn't see the internal drift, we can't pinpoint exactly when the process began to fail, forcing us to pull much larger batches than necessary.
- Erosion of Trust: Once a customer sees a "perfect" part fail due to an internal flaw we claimed was monitored, our credibility as a quality organization evaporates.
The avoided conversation about upgrading our sensing tech is uncomfortable because it requires investment and change. The delayed consequence—a public failure and a massive warranty claim—is usually expensive, public, and much harder to recover from. We are trading a manageable operational cost today for an unmanageable brand disaster tomorrow.
A New Operating System for Inspection: Capturing Coherence and Phase Data
To move past the Intensity Illusion, we have to change our "operating system" for how we view inspection data. This isn't about replacing every sensor on the floor overnight; it’s about integrating advanced sensing—specifically photonic-based acquisition—into the critical points of your process where material integrity is paramount.
We need to move from simple spot checks to full-spectrum capture. This means looking for coherence: how well do the different modes of a signal align? When those modes begin to overlap or drift, it tells us something about the internal state of the part that an intensity check will never reveal.
Here is the framework for this transition:
- Identify High-Stakes Nodes: Don't upgrade everything at once. Find the specific points in your process where "invisible" material shifts lead to field failures.
- Integrate Photonic Sensing: Deploy sensors capable of separating overlapping signal modes. This allows you to see the phase data, providing a high-resolution map of the part’s internal state.
- Establish Coherence Thresholds: Just as you have torque specs or oven temperatures, you must establish "coherence limits." If the signal phase drifts beyond a certain point, the part is flagged—even if its intensity looks perfect.
- Close the Feedback Loop: Feed this high-resolution data back to R&D and production. Use it to identify exactly where in the process the material begins to drift.
Making Advanced Sensing Part of Daily Work Tomorrow
Moving from theory to the shop floor requires a shift in how we train our teams and audit our processes. You can start making these changes this week by focusing on three areas:
Audit Your Current Sensors: Walk the line and ask your operators: "What does this number actually tell us about the part's health?" If the answer is only "it looks good," you have a data gap that needs to be filled.
Update Reaction Plans: For every critical inspection point, ensure there is a reaction plan taped to the machine or embedded in the software. This plan should specify what happens when signal coherence—not just intensity—drifts out of bounds.
Engage R&D on "Signal Integrity": In your next meeting with engineering, move the conversation away from "pass/fail" rates and toward "signal integrity." Ask them how we can better see the internal physical states that precede a failure.
Start by identifying one high-risk component where you’ve seen field failures despite passing line inspections. That is your pilot project for photonic integration.
Conclusion & Next Steps in the Taboos Series
The truth about our quality issues is often hidden in the noise we choose to ignore. We have spent years perfecting the art of measuring what is easy to see, while the most critical failures happen in the spaces where our sensors are currently blind. By adopting a more sophisticated way of looking at signal data—moving from intensity to coherence—we take ownership of the "hidden" variables that actually dictate our success.
Quality is not an accident; it's a discipline of seeking out the truth, even when that truth requires better tools and harder questions.
In the next installment of our Corporate Taboos series, we will look at why most organizations intentionally choose to ignore these "invisible" data points during the budget cycle, and how you can build a business case for visibility over vanity metrics.
Download and Share This Issue
Next Issue Preview
Next week, we examine the taboo of ‘The Optimized Process Myth’—the belief that merely making things faster automatically makes them better.
Call to Action
What process data are you still treating as 'good enough' because it was hard to measure? Share this with a peer who needs to think bigger about their inspection plans. | [email protected]
Newsletter replies and questions: [email protected]
Follow updates on X.com: @kaizen6sigma
References
Photonic chip separates three modes of mixed light to reveal hidden details in imaging (Source: interestingengineering.com)